Industrial Chemical Manufacturers Guide With Chemical Production and Industry Insights
Industrial chemical manufacturers are an important part of modern production because chemicals are used across agriculture, construction, electronics, textiles, food processing, automotive production, energy, water treatment, and many other industries.
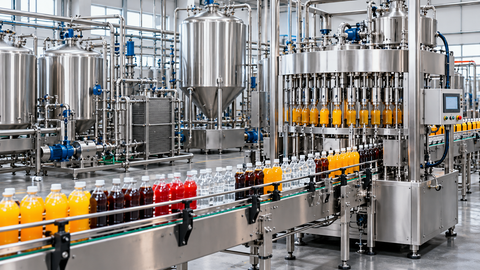
Chemical production converts raw materials into substances with defined physical and chemical properties for use in industrial processes and finished products. Industrial chemical manufacturers operate facilities where materials are processed, reacted, separated, purified, blended, packaged, and stored under controlled conditions.
Context
What Industrial Chemical Manufacturers Do
Industrial chemical manufacturers produce a wide range of substances, from basic industrial chemicals and solvents to polymers, coatings, additives, gases, acids, alkalis, and specialty chemical formulations. Some facilities focus on large-volume chemicals, while others concentrate on materials designed for specific manufacturing applications.
Chemical production generally begins with selected raw materials. Depending on the chemical involved, these materials can include minerals, natural resources, gases, agricultural materials, petroleum-derived feedstocks, or previously manufactured chemical intermediates.
The production process can include several stages:
- Raw material preparation involves checking, measuring, and conditioning incoming materials.
- Chemical reactions transform materials into new substances under controlled conditions.
- Separation removes unwanted components from the resulting mixture.
- Purification improves the consistency and required chemical properties.
- Blending combines materials according to a defined formulation.
- Quality testing verifies whether the finished material meets established specifications.
- Packaging and storage protect materials from contamination, moisture, heat, or other environmental factors.
Main Categories of Chemical Production
Industrial chemical manufacturers can be grouped according to the type of materials they produce. Basic chemicals are generally manufactured in large quantities and become inputs for other industrial processes. Specialty chemicals are usually developed around particular performance characteristics or applications.
Other important categories include polymers and resins, industrial gases, inorganic chemicals, organic chemicals, agricultural chemicals, coatings and additives, electronic chemicals, water-treatment chemicals, and chemical intermediates.
The distinction between these categories helps explain why chemical production facilities can have very different equipment, process designs, energy requirements, and quality-control systems.
How Chemical Manufacturing Developed
Modern chemical manufacturing expanded alongside industrialization because manufacturers needed consistent quantities of materials for large-scale production. Improvements in reaction engineering, process control, materials science, and analytical testing gradually allowed chemical facilities to operate with greater consistency and tighter process control.
Today, industrial chemical manufacturers increasingly combine traditional chemical engineering with automation, digital monitoring, advanced sensors, data analysis, and environmental management systems.
Importance
Why Chemical Manufacturers Matter
Chemical production supports numerous industries that people encounter in everyday life. Paints, adhesives, plastics, construction materials, textiles, packaging, electronic components, cleaning formulations, and many other products depend on chemical inputs at some stage of production.
Industrial chemical manufacturers also support infrastructure and industrial processes. Chemicals may be involved in water purification, metal processing, paper production, semiconductor manufacturing, energy generation, and material finishing.
Who Is Affected
The chemical manufacturing industry affects several groups:
- Manufacturers depend on consistent chemical inputs for production processes.
- Workers interact with chemical materials, processing equipment, storage systems, and safety procedures.
- Communities located near industrial facilities may be affected by transportation, environmental controls, and facility operations.
- Consumers encounter chemical-derived materials in products used at home, in transportation, construction, communications, and other areas.
- Environmental authorities oversee emissions, waste handling, chemical storage, and other potential environmental impacts.
Production Challenges
Chemical production requires careful management because different substances can react with one another or change behavior under different temperatures, pressures, concentrations, or storage conditions.
Common operational challenges include maintaining consistent product specifications, controlling energy use, managing hazardous materials, preventing contamination, reducing waste, and maintaining reliable process conditions.
Modern facilities therefore use process instrumentation, automated controls, laboratory analysis, equipment inspections, and documented operating procedures to manage production conditions.
Recent Updates
Automation and Digital Process Control
From 2024 through 2026, chemical manufacturing has continued moving toward greater use of automation and digital process monitoring. Sensors can continuously measure variables such as temperature, pressure, flow, level, and chemical composition.
Digital control systems can collect this information and display process conditions to operators. Data analysis can also help identify unusual operating patterns and support equipment maintenance planning.
Energy and Resource Efficiency
Energy management has become an increasingly important consideration for chemical production. Many chemical processes require substantial heat, cooling, compression, or separation.
Manufacturers are therefore examining heat recovery, improved process integration, efficient equipment, electrification, renewable electricity, and process optimization. Resource efficiency can also involve reducing water consumption and recovering useful materials from process streams.
Circular Chemical Production
Another developing trend is greater attention to circular production models. These approaches examine how chemical materials, polymers, solvents, and other industrial inputs can be recovered, reused, recycled, or incorporated into new production pathways.
Chemical recycling and advanced material recovery are being investigated for applications where conventional mechanical recycling may have limitations. The practical approach depends on the material, process chemistry, energy requirements, and environmental conditions.
Data Table
| Area | Traditional Approach | Current Industry Direction |
|---|---|---|
| Process monitoring | Periodic measurements | Continuous digital monitoring |
| Equipment maintenance | Scheduled maintenance | Condition-based planning |
| Quality control | Laboratory testing | Laboratory and in-process analysis |
| Energy management | Basic consumption tracking | Process integration and efficiency analysis |
| Production records | Paper or isolated systems | Integrated digital records |
| Material management | Linear material flow | Greater recovery and circularity |
| Safety monitoring | Manual inspections | Sensors, alarms, and automated controls |
Laws or Policies
Chemical Safety Requirements
Chemical manufacturing is shaped by regulations concerning worker protection, environmental impacts, chemical classification, transportation, storage, labeling, waste handling, and emergency preparedness. The exact requirements differ between jurisdictions.
A major international approach is the Globally Harmonized System of Classification and Labelling of Chemicals, commonly known as GHS. It provides a framework for communicating chemical hazards through labels and safety data information.
Environmental Controls
Industrial facilities may be subject to rules covering air emissions, wastewater discharge, hazardous waste, chemical storage, and accidental releases. Regulatory systems generally require manufacturers to identify potential environmental impacts and maintain appropriate controls.
Requirements can include emissions monitoring, waste documentation, facility inspections, environmental reporting, and emergency response planning. The specific obligations depend on the substances, production capacity, location, and applicable legislation.
Chemical Registration and Assessment
Several jurisdictions maintain systems for registering, evaluating, restricting, or controlling chemicals. These systems can require information about chemical identity, hazards, exposure, production, handling, and intended uses.
International chemical manufacturers may therefore need to maintain detailed technical documentation and supply-chain information. Changes in chemical regulations can also affect material selection, labeling, formulations, and production procedures.
Workplace Protection
Worker protection rules commonly address exposure limits, personal protective equipment, ventilation, machine safety, chemical handling, training, emergency procedures, and hazard communication.
Chemical facilities typically establish documented procedures for handling materials and responding to spills, leaks, equipment failures, fires, or other abnormal conditions. Professional requirements vary according to the jurisdiction and type of facility.
Tools and Resources
Chemical Process Simulation
Process simulation software can model chemical reactions, material flows, heat balances, separation systems, and equipment conditions. These tools are commonly used during process design, analysis, and optimization.
Laboratory and Analytical Equipment
Analytical instruments help determine chemical composition and product characteristics. Common technologies include chromatography, spectroscopy, titration systems, moisture analysis, particle measurement, and physical-property testing.
Safety Data Resources
Safety data sheets provide information about chemical hazards, handling, storage, exposure controls, emergency measures, and physical properties. They are an important reference for workers and organizations handling industrial chemicals.
Production Management Systems
Manufacturing execution systems and enterprise resource planning platforms can help manage production records, inventory, quality information, maintenance activities, and material tracking.
Reference and Planning Tools
Useful resources for chemical manufacturing may include:
- Chemical property databases
- Process safety checklists
- Production calculation worksheets
- Equipment maintenance schedules
- Chemical compatibility charts
- Risk assessment templates
- Environmental monitoring records
- Quality-control documentation
- Safety data sheet management systems
These tools help organize technical information and support consistent industrial processes.
FAQs
What do industrial chemical manufacturers produce?
Industrial chemical manufacturers produce basic chemicals, specialty chemicals, polymers, solvents, industrial gases, additives, coatings, chemical intermediates, and many other materials used by manufacturing industries.
How does chemical production work?
Chemical production can involve raw material preparation, controlled reactions, separation, purification, blending, testing, and packaging. The exact sequence depends on the chemical and its intended industrial application.
Why are industrial chemical manufacturers important?
Industrial chemical manufacturers provide materials used across construction, automotive production, electronics, textiles, packaging, energy, agriculture, water treatment, and numerous other industrial activities.
What technologies are used by chemical manufacturers?
Common technologies include process control systems, industrial sensors, laboratory analysis equipment, process simulation software, automated equipment, digital monitoring platforms, and manufacturing management systems.
What regulations affect chemical production?
Chemical production is influenced by rules covering chemical classification, worker protection, environmental emissions, waste management, transportation, storage, labeling, and emergency response. Requirements vary by jurisdiction and chemical category.
Conclusion
Industrial chemical manufacturers form an important part of global industrial infrastructure by converting raw materials into chemicals used across numerous manufacturing sectors. Modern chemical production increasingly combines process engineering with automation, digital monitoring, resource efficiency, and structured safety management. Regulatory systems also play an important role in controlling chemical hazards, environmental impacts, labeling, storage, and workplace exposure. Understanding these areas provides useful context for how chemical manufacturing operates and how the industry continues to develop.