Predictive Maintenance Systems Explained With Sensors, Data Analytics, and Monitoring
Predictive maintenance systems use sensors, data analytics, and equipment monitoring to identify possible machine problems before they cause unexpected breakdowns. This approach helps industrial facilities understand the condition of machinery while it operates.
Instead of relying only on fixed maintenance schedules or waiting for equipment to fail, predictive maintenance uses measured information to estimate when maintenance may be necessary.
The concept developed from traditional equipment inspection, mechanical engineering, and industrial condition monitoring. Earlier maintenance practices often depended on manual inspections, operating experience, and scheduled component replacements. As digital sensors, computing systems, and industrial communication technologies developed, manufacturers gained more ways to collect and analyze equipment data continuously.
Predictive maintenance is now associated with industrial automation, manufacturing plants, energy facilities, transportation systems, and commercial buildings. It can monitor equipment such as electric motors, pumps, compressors, turbines, conveyor systems, and heating and cooling units.
How Predictive Maintenance Systems Work
A predictive maintenance system collects operating information, evaluates changes in equipment behavior, and identifies patterns associated with potential faults. Maintenance teams can use these findings to investigate developing problems before equipment performance deteriorates significantly.
The process generally involves four stages:
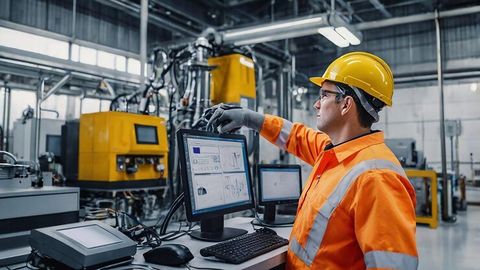
Data collection: Sensors measure vibration, temperature, pressure, electrical current, speed, or other operating conditions.
Data transmission: Industrial networks transfer measurements to a monitoring platform or local computing system.
Data analysis: Software evaluates current readings against historical patterns, operating limits, and equipment performance.
Maintenance planning: Technical personnel investigate alerts and determine whether inspection, adjustment, or component replacement is necessary.
For example, a pump with increasing vibration may have a developing alignment problem or a worn bearing. Monitoring the change over time can help maintenance personnel investigate the cause before the pump experiences a major failure.
Predictive Maintenance Compared With Other Approaches
Predictive maintenance differs from other maintenance strategies because it considers actual equipment condition and potential failure patterns.
Maintenance approach | Main principle | Typical application |
|---|---|---|
Reactive maintenance | Repair equipment after failure | Noncritical equipment with limited consequences |
Preventive maintenance | Perform maintenance at planned intervals | Equipment requiring routine inspection |
Predictive maintenance | Analyze condition data to anticipate problems | Machinery with measurable operating patterns |
Prescriptive maintenance | Evaluate possible actions using analytical models | Complex equipment and connected industrial systems |
These approaches can operate together within one facility. A maintenance program may use scheduled inspections for some components, condition monitoring for critical machinery, and reactive repairs for equipment where failure has limited operational consequences.
Importance
Predictive maintenance matters because unexpected equipment failures can interrupt production, affect product quality, increase material waste, and create safety concerns. A malfunctioning machine can also affect connected production stages, making a relatively small technical problem more disruptive across an entire facility.
Manufacturers, facility managers, utilities, transportation operators, and equipment maintenance teams use predictive maintenance to improve their understanding of machinery condition. Its relevance has increased as industrial systems become more automated and equipment performance depends on interconnected components.
Problems Addressed by Equipment Monitoring
One important application is reducing uncertainty about machine condition. A machine may continue operating even when a bearing, belt, electrical connection, or lubrication system begins to deteriorate. Visual inspection alone may not identify every developing issue, particularly when components are enclosed or operate continuously.
Predictive maintenance can help address several common challenges:
Unexpected breakdowns: Changes in vibration, temperature, or current may indicate a developing fault.
Unplanned production interruptions: Early warnings can help maintenance teams coordinate inspections with production schedules.
Equipment deterioration: Historical measurements can reveal gradual changes that are difficult to identify through occasional inspections.
Spare-parts planning: Condition information can support decisions about which components may require attention.
Workplace safety: Identifying certain mechanical or electrical abnormalities can help personnel investigate potentially hazardous conditions.
These benefits depend on sensor quality, equipment characteristics, accurate interpretation, and appropriate maintenance procedures. A monitoring alert does not automatically confirm a fault, and not every failure can be predicted in advance.
Who Uses Predictive Maintenance Systems?
Predictive maintenance is relevant to industries with equipment that operates for extended periods or performs essential tasks. The specific monitoring methods depend on operating conditions and the consequences of equipment failure.
Manufacturing facilities may monitor production lines, industrial robots, gearboxes, and machine tools. Energy operators may assess turbines, generators, transformers, and pumps. Commercial buildings may use monitoring systems to evaluate ventilation equipment, chillers, elevators, and other mechanical assets.
Smaller organizations can also use condition monitoring for selected critical equipment without connecting every machine to a large industrial analytics platform. The appropriate level of monitoring depends on technical requirements, operational priorities, and the availability of reliable data.
Recent Updates
Recent developments in predictive maintenance have focused on artificial intelligence, connected sensors, edge computing, and more integrated industrial monitoring platforms. These technologies are changing how organizations collect, interpret, and use equipment information.
Artificial Intelligence and Machine Learning
Machine learning models can analyze large collections of equipment measurements to identify patterns associated with abnormal operation. Depending on the available data, these models may detect unusual vibration, identify changes in energy consumption, or estimate the likelihood of particular failure types.
AI-based predictive maintenance can be useful when equipment behavior is influenced by several variables at once. However, model accuracy depends on representative training data, reliable measurements, and appropriate validation. Unusual operating conditions or changes in machinery configuration can produce misleading results.
Industrial Internet of Things and Connected Sensors
The Industrial Internet of Things, commonly called IIoT, connects machinery, sensors, controllers, and monitoring software through industrial communication networks. Connected equipment can provide information about operating temperature, vibration, pressure, energy use, and production conditions.
Wireless sensors have also expanded monitoring options for machinery where installing extensive wiring would be difficult. Nevertheless, battery life, signal interference, network reliability, and cybersecurity remain important considerations.
Edge Computing and Cloud Analytics
Edge computing processes data close to the machinery instead of sending every measurement to a remote platform. This arrangement can support rapid alerts and reduce the volume of information transmitted across a network.
Cloud analytics can support longer-term data storage, comparisons between facilities, and more computationally demanding analysis. Some systems combine both approaches, using local processing for immediate monitoring and centralized platforms for historical analysis.
Digital Twins and Equipment Health Models
A digital twin is a digital representation of a physical asset or process that uses operational information to describe its behavior. When properly configured, it can help engineers compare actual equipment performance with expected operating conditions.
Digital twins can support maintenance planning, fault investigation, and operating scenario analysis. Their usefulness depends on how accurately the digital representation reflects the real equipment and how frequently its underlying information is updated.
Laws or Policies
Predictive maintenance systems are influenced by workplace safety requirements, machinery regulations, electrical safety rules, data protection obligations, and cybersecurity policies. Requirements differ by country, industry, equipment category, and the potential consequences of failure.
In India, industrial maintenance practices may be affected by applicable occupational safety legislation, factory safety requirements, electrical regulations, environmental rules, and sector-specific technical standards. The Occupational Safety, Health and Working Conditions Code, 2020, forms part of the country's occupational safety legislative framework. Its implementation and applicable requirements should be checked against current official government notifications and the relevant workplace circumstances.
Equipment Safety and Technical Standards
Technical standards can provide guidance on machinery condition monitoring, vibration measurement, asset management, and reliability engineering. The ISO 17359 standard, for example, addresses general procedures for machinery condition monitoring and diagnostics. ISO 55000 provides principles and terminology relating to asset management.
Such standards may support the design of maintenance programs, but their relevance depends on the equipment, organizational requirements, and applicable legal obligations. A standard does not automatically become a legal requirement in every location.
Data Protection and Industrial Cybersecurity
Connected monitoring platforms may collect operational data that organizations consider confidential. Systems that integrate with employee information, access records, or other personal data may also be subject to applicable privacy requirements.
Industrial networks require appropriate access controls, secure communications, software updates, backups, and procedures for responding to security incidents. Maintenance systems should be configured so that monitoring functions do not create unnecessary exposure for production equipment or connected networks.
Organizations remain responsible for meeting applicable safety and legal requirements even when predictive analytics or automated alerts are used.
Tools and Resources
Predictive maintenance depends on a combination of measurement hardware, analytical software, historical records, and maintenance planning tools. The selection depends on machinery type, monitoring objectives, available technical skills, and existing industrial infrastructure.
Common Predictive Maintenance Tools
The following table summarizes commonly used tools and their roles in an industrial monitoring program.
Tool or resource | Primary function | Example application |
|---|---|---|
Vibration sensors | Measure mechanical movement | Detecting changes in motors and bearings |
Temperature sensors | Monitor heat levels | Identifying overheating in motors or gearboxes |
Pressure sensors | Measure fluid or gas pressure | Monitoring pumps and compressed-air systems |
Current sensors | Measure electrical current | Identifying changes in motor operating behavior |
Data acquisition systems | Collect measurements from equipment | Recording readings from multiple sensors |
Condition monitoring software | Display readings and generate alerts | Reviewing equipment health trends |
Machine learning platforms | Analyze patterns in historical data | Identifying unusual operating behavior |
Computerized maintenance management systems (CMMS) | Organize maintenance records and work orders | Tracking inspections, repairs, and component history |
Selecting a Monitoring Platform
A suitable monitoring platform should support the equipment being assessed and the measurements needed for meaningful analysis. Compatibility with existing controllers, industrial communication protocols, sensor hardware, and maintenance records can affect implementation.
Important evaluation factors include:
Data accuracy: Measurements should be suitable for the intended monitoring task.
Alert configuration: Thresholds should reflect operating conditions and equipment requirements.
Historical records: The system should retain enough information to compare current and previous performance.
Integration: Relevant information should be accessible to maintenance and operations personnel.
Security: Access controls and network protections should match the operational risks.
Reporting: Results should be understandable to people responsible for investigating and resolving equipment problems.
Maintenance Records and Analytical Resources
Historical maintenance records help explain whether unusual measurements correspond to known mechanical problems. Inspection reports, component replacement histories, operating logs, and fault records can improve the interpretation of sensor data.
Trend charts, vibration analysis reports, equipment manuals, and reliability calculations can also support maintenance decisions. These resources are most useful when measurements are recorded consistently and analyzed alongside relevant operating conditions.
FAQs
What Is a Predictive Maintenance System?
A predictive maintenance system uses equipment sensors, historical records, and data analytics to identify signs of deterioration. It helps maintenance personnel assess when an inspection or repair may be needed.
How Do Sensors Support Predictive Maintenance?
Sensors measure conditions such as vibration, temperature, pressure, and electrical current. Monitoring software evaluates these measurements to identify unusual patterns that may indicate a developing equipment problem.
What Is AI-Based Predictive Maintenance?
AI-based predictive maintenance uses machine learning or related analytical techniques to recognize equipment behavior patterns. Depending on data quality and model validation, it can help identify abnormalities and estimate potential failure risks.
Which Industries Use Predictive Maintenance Systems?
Manufacturing, energy, transportation, mining, utilities, and commercial building operations use predictive maintenance for selected machinery and infrastructure. Applications vary according to equipment criticality and monitoring requirements.
What Is the Difference Between Preventive and Predictive Maintenance?
Preventive maintenance follows a planned schedule, such as an inspection every few months. Predictive maintenance uses equipment condition data to help determine when maintenance may be appropriate.
Conclusion
Predictive maintenance systems combine sensors, equipment monitoring, and data analytics to identify possible machinery problems before they develop into serious disruptions. Artificial intelligence, connected industrial devices, and edge computing are expanding the ways organizations analyze equipment condition. Effective implementation depends on reliable measurements, suitable analytical methods, trained personnel, and compliance with applicable safety and cybersecurity requirements. Predictive maintenance complements other maintenance approaches rather than eliminating the need for inspections and technical judgment.