Industrial Chemical Plants Guide With Processing Technology and Engineering Insights
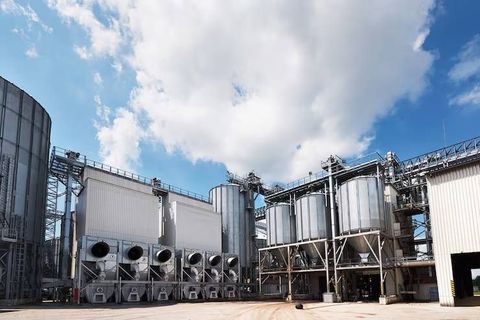
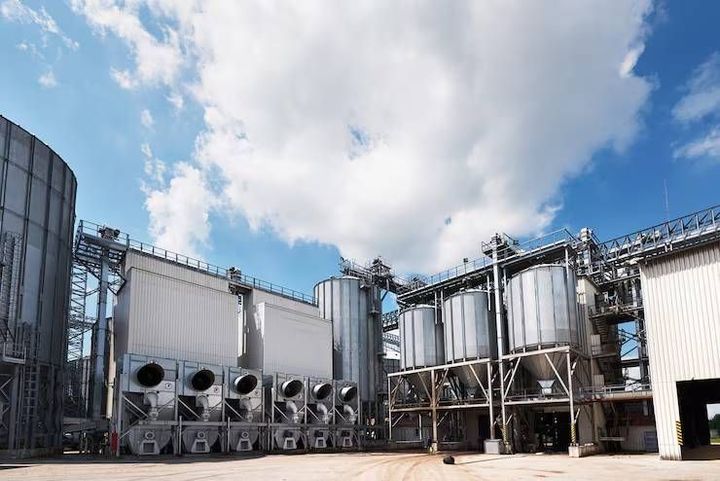
Industrial chemical plants are specialized facilities designed to transform raw materials into chemicals, intermediate compounds, fuels, polymers, coatings, fertilizers, and other industrial materials. Industrial chemical plants combine chemical reactions, separation systems, heat transfer equipment, storage units, process controls, and safety systems within an integrated production environment.
Modern chemical processing technology also uses automation, sensors, digital monitoring, and energy management to improve process consistency and environmental performance.
Understanding industrial chemical plants is useful because chemical processing supports many products used in everyday life. Materials for construction, agriculture, electronics, packaging, transportation, healthcare, textiles, and household products can originate from chemical processing facilities. The design of these plants requires coordination between chemical engineering, mechanical engineering, electrical systems, instrumentation, environmental controls, and industrial safety.
Context
What Industrial Chemical Plants Do
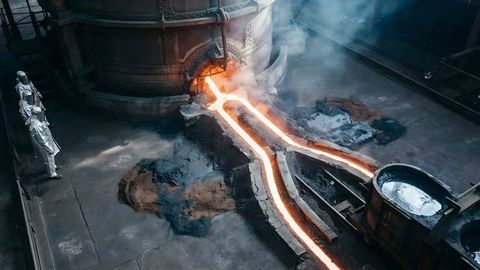
An industrial chemical plant converts selected feedstocks into useful chemical materials through controlled physical and chemical processes. Depending on the plant type, the feedstock may include minerals, gases, petroleum-derived materials, agricultural inputs, recycled materials, or other chemical compounds.
A typical process can include several connected stages:
- Raw material preparation involves receiving, measuring, filtering, drying, crushing, mixing, or otherwise conditioning feedstocks.
- Chemical reaction involves controlled changes in molecular structure through heat, pressure, catalysts, electricity, or other process conditions.
- Separation removes unwanted materials or divides a mixture into useful components.
- Purification improves the composition of the desired product through methods such as distillation, filtration, crystallization, absorption, or membrane separation.
- Storage keeps raw materials, intermediate materials, and finished chemical products in appropriate tanks, vessels, silos, or specialized containers.
The exact arrangement depends on the chemistry involved, required production capacity, physical properties of materials, and environmental requirements.
Main Engineering Systems
Chemical plant engineering involves many interconnected systems rather than one individual machine. Process equipment may include reactors, heat exchangers, pumps, compressors, evaporators, dryers, mixers, filters, distillation columns, storage tanks, and piping networks.
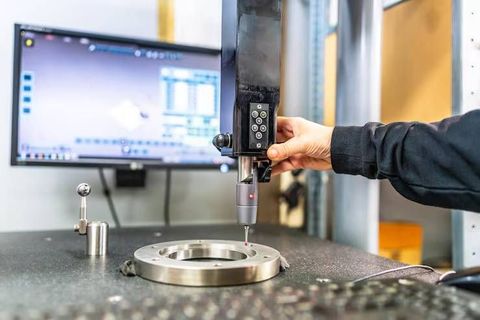
Instrumentation is equally important. Temperature, pressure, flow, level, composition, and other variables can be measured continuously. Control systems then use this information to regulate valves, pumps, heating systems, cooling equipment, and other process components.
Electrical infrastructure supplies power to motors, control systems, lighting, monitoring equipment, and specialized machinery. Mechanical structures support equipment and piping, while ventilation and containment systems help manage process conditions and potential releases.
Common Types of Chemical Plants
Industrial chemical plants can be categorized according to the materials they process and the technologies they use.
| Plant Category | Typical Processing Activities | Common Output Areas |
|---|---|---|
| Petrochemical plants | Cracking, reforming, separation | Chemical intermediates and polymers |
| Fertilizer plants | Synthesis, reaction, granulation | Agricultural nutrients |
| Polymer plants | Polymerization, blending, extrusion | Plastics and synthetic materials |
| Specialty chemical plants | Mixing, reaction, purification | Coatings, additives, formulated chemicals |
| Inorganic chemical plants | Reaction, precipitation, crystallization | Industrial mineral compounds |
| Biochemical plants | Fermentation, separation, purification | Biological and biochemical materials |
| Recycling chemical plants | Recovery, separation, purification | Recovered chemical feedstocks |
Some facilities perform a single major transformation, while integrated industrial complexes can contain multiple processing units connected through shared utilities and infrastructure.
Importance
Role in Everyday Industries
Chemical plants affect a wide range of industries because chemical materials are often intermediate inputs rather than final consumer products. Plastics used in packaging, coatings applied to buildings, materials used in electronic components, and chemicals used in water treatment can all depend on industrial chemical processing.
Chemical manufacturing also supports infrastructure and manufacturing activities. Adhesives, synthetic fibers, insulation materials, corrosion-resistant coatings, industrial gases, and processing chemicals are examples of materials that can be produced through specialized chemical operations.
Process Efficiency and Resource Management
Modern chemical plant engineering increasingly focuses on efficient use of raw materials, water, energy, and process equipment. Heat integration can allow energy from one process stream to support another process step. Process optimization can also reduce unnecessary material movement and improve control over operating conditions.
Water management is another important consideration. Industrial facilities may use water for cooling, cleaning, steam generation, and processing. Recycling and treatment systems can reduce the amount of fresh water required for repeated operations.
Industrial Safety
Chemical processing can involve high temperatures, elevated pressures, reactive substances, flammable materials, corrosive compounds, or toxic substances. For this reason, industrial chemical plants use layers of protection rather than relying on a single safety mechanism.
Common safety measures include:
- Pressure relief systems
- Emergency shutdown systems
- Gas and fire detection
- Containment structures
- Process alarms
- Ventilation systems
- Protective equipment
- Equipment inspection programs
- Emergency response procedures
Hazard identification is generally performed during plant design and continues through operation and maintenance activities.
Recent Updates
Automation and Digital Process Control
Recent development in industrial chemical plants has increasingly involved digital process control. Distributed control systems, programmable controllers, industrial sensors, and supervisory platforms can collect process information and help operators understand changing conditions.
Advanced analytics can examine historical and real-time process information to identify unusual patterns. Predictive maintenance techniques can also use equipment data to identify conditions that may require inspection before a mechanical problem interrupts production.
Artificial Intelligence and Process Optimization
Artificial intelligence and machine learning are being explored for process monitoring, equipment diagnostics, quality analysis, energy optimization, and production planning. These technologies generally work alongside established control systems rather than replacing the underlying engineering infrastructure.
Digital twins are another developing area. A digital representation of a process or equipment system can be used to examine operating scenarios, evaluate process changes, and support engineering analysis without directly changing the physical plant.
Environmental and Energy Improvements
Chemical processing is also moving toward greater attention to energy efficiency, emissions management, water reuse, waste reduction, and alternative feedstocks. Electrification of selected process equipment and integration of lower-carbon energy sources are being evaluated for processes where technical conditions allow.
Carbon capture, utilization, recycling technologies, improved catalysts, and chemical recovery systems are additional areas of development. Their practical application varies according to process chemistry, infrastructure, energy availability, and regulatory requirements.
Laws or Policies
Industrial Environmental Requirements
Industrial chemical plants are generally subject to environmental requirements covering air emissions, wastewater, hazardous materials, waste management, chemical storage, and emergency planning. The specific rules depend on the country, region, facility type, and chemicals involved.
Facilities may need environmental permits before construction or operation. Regulatory frameworks can also establish limits for emissions, discharge quality, waste handling, and reporting procedures.
Chemical Handling and Workplace Safety
Chemical plant regulations commonly address hazard communication, labeling, storage, transportation within facilities, exposure control, emergency procedures, and worker protection. Pressure vessels, electrical equipment, boilers, lifting systems, and other plant infrastructure may also be subject to technical inspection requirements.
Environmental and safety requirements can influence plant layout from the earliest engineering stages. Separation distances, containment areas, emergency access, ventilation, drainage, and monitoring systems may all be incorporated into the facility design.
Process Risk Management
Risk assessment is an important part of chemical plant engineering. Methods such as hazard and operability studies, layer-of-protection analysis, consequence assessment, and process safety reviews can be used to examine possible failure scenarios.
Regulatory programs differ across jurisdictions, but the general objective is to identify hazards, control risks, protect people and the environment, and maintain reliable operating procedures.
Tools and Resources
Engineering and Process Design Tools
Chemical engineers use process simulation software to model reactions, material balances, energy flows, separation processes, and equipment requirements. These tools can help engineers examine different process conditions during plant design and optimization.
Computer-aided design platforms are commonly used for plant layouts, piping arrangements, equipment drawings, structural designs, and three-dimensional facility models.
Monitoring and Control Platforms
Industrial control platforms collect information from field instruments and provide operators with process displays, alarms, trends, and control functions. Historian systems can retain operational information for analysis, reporting, troubleshooting, and process improvement.
Useful resources can include:
- Process simulation platforms
- Piping and instrumentation diagram tools
- Equipment sizing calculators
- Energy balance calculators
- Chemical compatibility databases
- Industrial safety templates
- Maintenance management platforms
- Environmental monitoring systems
- Process control dashboards
- Engineering standards databases
The appropriate tool depends on the chemical process, plant scale, engineering discipline, and regulatory environment.
FAQs
What are industrial chemical plants?
Industrial chemical plants are facilities that transform raw materials into chemical compounds and industrial materials through controlled physical and chemical processes. They may use reactors, separation equipment, heat exchangers, pumps, storage systems, and automated controls.
How does chemical processing technology work?
Chemical processing technology combines physical operations and chemical reactions to transform feedstocks into specified materials. Common stages include preparation, reaction, separation, purification, quality control, and storage.
What equipment is used in industrial chemical plants?
Common equipment includes reactors, distillation columns, heat exchangers, pumps, compressors, filters, mixers, dryers, evaporators, storage tanks, valves, and process instrumentation. Equipment selection depends on material properties and process conditions.
How is safety managed in chemical plants?
Safety is managed through equipment design, process controls, hazard assessment, emergency shutdown systems, pressure protection, containment, monitoring, maintenance, training, and emergency procedures. Multiple protective layers are normally used because chemical processes can involve different types of hazards.
What are current trends in chemical plant engineering?
Current trends include increased automation, digital process monitoring, predictive maintenance, artificial intelligence, energy optimization, water reuse, emissions management, advanced process control, and development of alternative feedstocks. Adoption varies according to technical and regulatory conditions.
Conclusion
Industrial chemical plants integrate chemical reactions, mechanical equipment, process controls, utilities, storage systems, and safety infrastructure to transform raw materials into useful industrial materials. Modern chemical plant engineering increasingly combines automation, digital monitoring, energy management, and environmental controls with established processing technologies. Regulations influence plant design, chemical handling, emissions management, waste treatment, and workplace protection. Understanding these interconnected systems provides useful context for how chemical processing supports manufacturing and many everyday industries.